7 Tips for Buying Chromium Carbide Overlay Plate?
Buying a Chromium Carbide Overlay Plate is not simply a matter of choosing the highest hardness number. The correct plate must match abrasion type, impact level, temperature, welding method, and available maintenance space. USGS Mineral Commodity Summaries 2025 shows that global chromium supply remains geographically concentrated. This matters because alloy chemistry, production consistency, and delivery risk can vary between suppliers.
Look beyond marketing claims. Ask for chemistry results, deposit thickness, hardness ranges, crack-pattern information, and test methods. ASTM G65 abrasion testing can help compare wear resistance, but laboratory results may not reproduce a crusher chute, cement mill, or mining hopper. Real conditions are messier. Plate selection should also consider weldability, heat input, distortion, and field repair requirements.
John C. Lippold, a recognized welding-metallurgy expert and author of Welding Metallurgy and Weldability, states, “Weldability is not an inherent material property, but rather a function of the material, fabrication process, and service conditions.” His point applies directly to overlay plate purchasing. A hard surface can still fail early if the backing plate is unsuitable or installation is poorly controlled. That mistake is expensive.
These seven tips focus on practical evidence: application mapping, alloy verification, dimensional tolerance, test standards, supplier experience, installation guidance, and total service cost. Compare more than price. Request traceable documents. Inspect the actual plate edge, weld profile, and surface cracking pattern before approval. No datasheet predicts every operating condition, so buyers should record field results and revise specifications when performance falls short.
Define Wear Conditions and Select ASTM G65 Testing Requirements
7 Tips for Buying Chromium Carbide Overlay Plate
Define the wear conditions before comparing chromium carbide overlay plates. Describe the abrasive, particle size, sliding speed, impact energy, temperature, and moisture. A conveyor handling dry quartz creates different damage from a chute carrying wet coal. Plate thickness also matters when impact may bend or crack the base metal.
ASTM G65 testing helps measure dry-sand rubber-wheel abrasion, but the procedure must match the purchasing purpose. Procedure A is severe, while other procedures may support different comparison levels. Never compare mass-loss values from different procedures as if they were equal. Request the test procedure, abrasive specification, wheel condition, load, test duration, and reported mass loss. Details matter.
Check the test report carefully. A lower mass loss usually indicates better resistance, but it does not guarantee longer service in every installation. ASTM G65 does not reproduce heavy impact, corrosion, heat cycling, or large trapped particles. That limitation is important. I have seen buyers select a plate from one impressive number, then overlook weld cracking or poor fit-up. This is where the decision becomes less certain. Ask for hardness mapping, overlay thickness, crack guidance, and base-plate information. Compare laboratory results with actual failure photos, shutdown records, and measured wear depth. A controlled field trial may reveal more than a polished data sheet.
Compare Chromium and Carbon Levels: Typical Ranges of 20–35% Cr and 3–5% C
7 Tips for Buying Chromium Carbide Overlay Plate?
Chromium and carbon levels deserve close attention when buying overlay plate. Technical references, including ASM Handbook Volume 18, commonly describe Fe-Cr-C wear alloys with approximately 20–35% chromium and 3–5% carbon. These elements form hard chromium carbides inside a tougher iron-based matrix. Higher chromium may improve resistance to severe mineral abrasion, but chemistry alone cannot predict service life.
Ask for a heat analysis, not only a brochure range. Optical emission spectroscopy can verify chromium and major alloying elements, while combustion analysis measures carbon more accurately. ASTM G65 test results can support abrasion comparisons, although laboratory rubber-wheel results may not match wet slurry or impact conditions. Check the actual deposit, because dilution from the base plate can lower carbon and chromium near the fusion line.
Plate thickness, crack pattern, carbide distribution, and weld quality also matter. A 6 mm overlay with uneven hardness may fail sooner than a thinner, consistent deposit. Typical hardness values often fall around 55–65 HRC, but test location changes the result. I would not accept hardness figures without a stated method, such as ASTM E18 or ISO 6507-1. Chemistry is only one part of the purchase decision. It is easy to overvalue impressive percentages and overlook impact loading, distortion, or poor fit-up.
Chromium and Carbon Levels in Chromium Carbide Overlay Plate
Typical chromium carbide overlay plates contain approximately 20–35 wt% chromium and 3–5 wt% carbon. The chart compares the lower and upper ends of these commonly specified composition ranges.
Values are representative typical ranges for chromium carbide overlay materials; actual chemistry may vary by product specification and application.
Match Overlay Hardness of 55–65 HRC to Impact and Abrasion Risks
7 Tips for Buying Chromium Carbide Overlay Plate
Selecting chromium carbide overlay plate starts with the working failure, not a catalog number. For severe sliding abrasion, 55–65 HRC usually offers useful resistance. However, higher hardness does not automatically mean longer service life. Consider impact energy, particle size, temperature, and contact pressure before choosing the plate.
Measure the job. A conveyor transfer point with sharp rock needs different protection from a chute carrying fine sand. Repeated impact can crack an overly hard overlay, especially when the base plate receives sudden loads. In these areas, a balanced hardness near 55–60 HRC may perform better. For steady mineral sliding, 60–65 HRC can be more suitable. Watch the edges.
Ask how hardness was tested. Surface readings can vary with carbide distribution, test location, and preparation quality. Request test records, overlay chemistry, plate thickness, and substrate details. Check whether the supplier controls dilution during welding, because inconsistent dilution may create uneven wear resistance. This detail is easy to overlook.
Fit also matters. Verify cutting limits, bending requirements, weld procedures, and operating temperature. A plate that resists abrasion but cannot be installed accurately creates costly gaps and stress points. I have seen specifications focus heavily on HRC while ignoring mounting conditions. That approach looks precise, but it can fail in the field. Build a small trial section when the duty cycle is uncertain, then inspect wear patterns after real production hours.
Confirm Plate Thickness, Commonly 3–30 mm, and Dimensional Tolerances
7 Tips for Buying Chromium Carbide Overlay Plate?
Plate thickness deserves more attention than the advertised number. Chromium carbide overlay plate is commonly supplied from 3–30 mm, but this may include both base steel and hardfacing layers. Ask the supplier to state each layer separately. A “10 mm plate” could mean 6 mm base steel plus 4 mm overlay. That difference affects weight, welding preparation, and service life. ASTM A6/A6M provides dimensional guidance for steel plate, while EN 10029 defines thickness tolerance classes for hot-rolled products. These standards do not automatically guarantee a perfectly uniform overlay.
Request a dimensional inspection report with actual readings from several points. Check thickness near the corners, center, and weld beads. Surface waviness can make one measurement misleading. For a 3–30 mm product, even a small deviation can affect chute gaps, bolt alignment, or replacement fitting. The World Steel Association reported 1,882.6 million tonnes of crude steel production in 2023, showing the scale of steel supply, but volume does not replace inspection. I would also confirm length, width, flatness, and cutting tolerances in writing. A practical mistake is accepting “standard tolerance” without defining the standard. It sounds professional, but it is incomplete. Also, overlay thickness may vary intentionally. That is not always a defect, yet it should match the drawing and wear conditions.
7 Tips for Buying Chromium Carbide Overlay Plate: Confirm Plate Thickness, Commonly 3–30 mm, and Dimensional Tolerances
| Tip | Purchase Dimension | Realistic Technical Guidance | What to Confirm Before Ordering | Why It Matters |
|---|---|---|---|---|
| 1 | Confirm total plate thickness | Chromium carbide overlay plate is commonly supplied in total thicknesses of approximately 3–30 mm. The total thickness normally includes the carbon-steel base plate plus the welded overlay. | State the required total thickness and identify the base thickness and overlay thickness separately, for example: 8 mm base + 5 mm overlay = 13 mm total. | Separating the two layers prevents confusion between the structural thickness and the wear-resistant working layer. |
| 2 | Define the dimensional tolerances | Thickness, length, width, flatness, and cut dimensions do not have one universal tolerance for every overlay plate. Tolerances depend on the base plate, welding process, heat input, plate size, and finishing method. | Request a written tolerance table. As a practical inquiry example, ask the supplier to state whether thickness is controlled by a specified positive/negative tolerance, whether cut dimensions are saw-cut or flame-cut, and how flatness is measured. | Overlay welding can create heat distortion and local thickness variation; agreed inspection rules make acceptance objective. |
| 3 | Check the base-plate grade | The base plate is commonly a weldable carbon or low-alloy steel selected for structural support and fabrication. Its chemical composition and mechanical properties are different from those of the chromium-carbide deposit. | Specify the required base-steel grade or minimum properties, including yield strength, tensile strength, impact requirements where applicable, and weldability documentation. | The base plate carries loads and determines how easily the product can be cut, formed, welded, or bolted. |
| 4 | Evaluate overlay chemistry and hardness | Chromium carbide overlays typically contain chromium and carbon in an iron-based weld deposit. Hardness is commonly reported in HRC or HV, but results vary with deposit chemistry, dilution, test location, and test method. | Request the nominal chemical range, hardness range, test method, number of test points, and whether the reported value applies to the deposit surface or a cross-section. | Hardness alone does not fully describe wear performance; chemistry, carbide distribution, impact conditions, and operating material must also be considered. |
| 5 | Match the plate to the wear mechanism | Chromium carbide overlay is widely used for abrasive sliding and gouging conditions. It may be unsuitable for severe impact, heavy forming, or applications requiring extensive bending. | Describe the material being handled, particle size, temperature, impact level, sliding speed, moisture, corrosive exposure, and expected service life. | A wear plate selected for sliding abrasion may crack or fail prematurely when subjected to repeated high-impact loading or strong corrosion. |
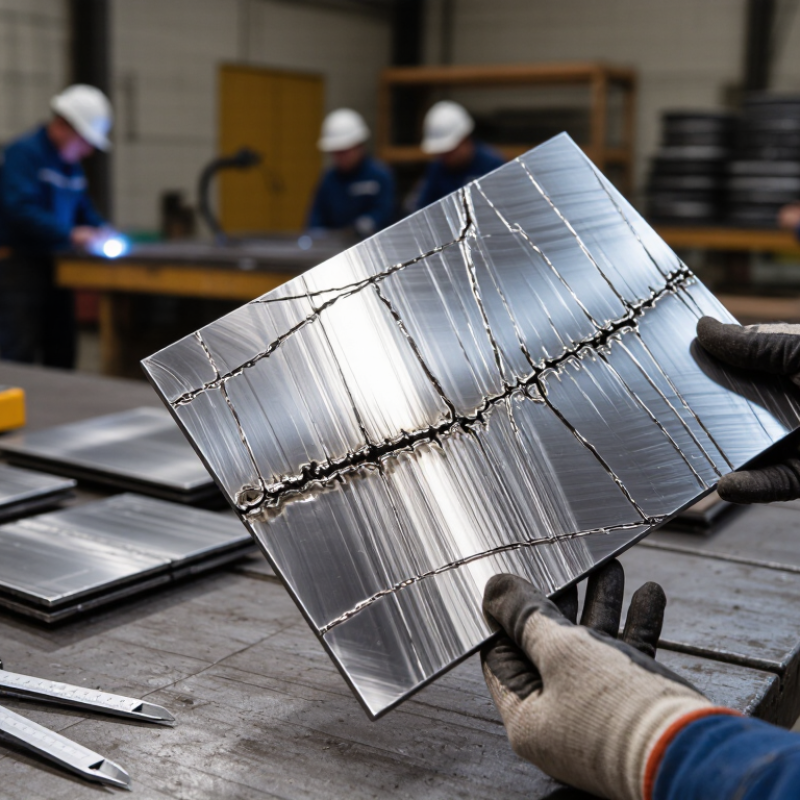
| 6 | Review cracks, bead pattern, and surface condition | Relief cracks across the overlay are commonly associated with stress release in hardfaced plate and are not automatically evidence of defective material. Crack spacing, crack width, penetration, and location should be evaluated against the agreed specification. | Confirm acceptable crack characteristics, overlay continuity, exposed base areas, surface profile, edge condition, and any grinding or machining allowance. | Controlled relief cracking can be normal, while excessive cracking, delamination, or exposed substrate can reduce usable wear life. |
| 7 | Verify inspection and delivery requirements | Important quality records may include dimensional inspection, visual inspection, hardness results, chemical analysis, base-material certificates, welding procedure information, and traceability records. | Specify plate quantity, finished dimensions, allowable distortion, marking, packaging, inspection documents, sample approval, and whether third-party inspection is required. | Clear documentation helps confirm that the delivered plate matches the approved design and makes replacement or quality claims easier to manage. |
Audit Welding Quality, Bond Integrity, Certifications, and Supplier Support
When buying chromium carbide overlay plate, do not judge quality from a polished sample alone. Ask how the welding process is controlled, recorded, and verified. A reliable supplier should provide weld procedure details, overlay chemistry, plate thickness, and dimensional tolerances. Inspect the surface for cracks, uneven beads, exposed base metal, and excessive porosity. Some transverse checking can be normal in hardfacing, but random deep cracks deserve investigation. Request recent inspection records, not generic claims. If possible, witness ultrasonic or dye penetrant testing on representative pieces. Small details matter.
Bond integrity needs more than a strong-looking surface. Ask how the overlay is attached to the steel backing and how bonding is tested. Cross-section samples can reveal lack of fusion, trapped slag, or inconsistent dilution. Compare test results with the intended impact, abrasion, and temperature conditions. A plate for coal chutes may fail quickly in hot clinker service. That mismatch is a purchasing error, not simply a material defect. I would also check cut edges and drilled holes, because poor fabrication can expose weak zones. Measure twice.
Certifications should be traceable to the actual production batch. Verify certificate numbers, testing laboratories, chemical analysis, and heat or lot identification. Supplier support also matters after delivery. Clarify cutting guidance, welding consumables, repair limits, lead times, packaging, and complaint response. Ask for installation references from similar service, but treat testimonials as supporting evidence only. A technically confident supplier will explain limitations without promising unlimited wear life. One uncomfortable question helps: what commonly goes wrong with this plate? The answer may expose more than a brochure. Keep written records of every promise.